Response Surface Methods for Casting Simulation: From Parameters to Zero-Defect Decisions
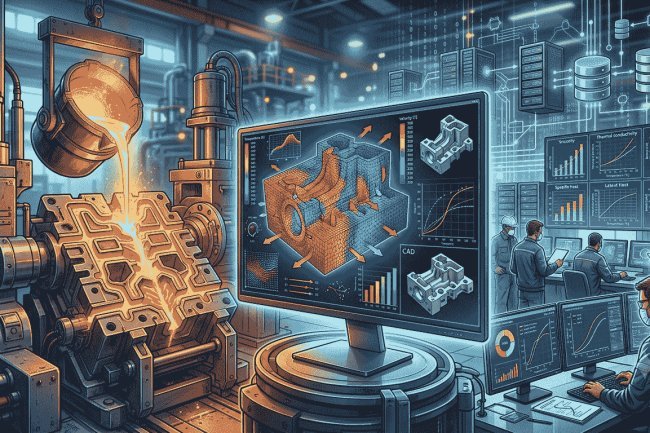
Modern foundries face an unrelenting pressure: deliver higher-quality castings faster, with less scrap, fewer physical trials, and tighter cost controls. Response Surface Methods (RSM) offer a rigorous, statistically grounded framework that transforms simulation outputs into actionable, decision-ready process maps. This presentation explores how RSM — combined with Design of Experiments (DoE) and digital twin infrastructure — enables casting engineers to navigate complex, multi-variable process spaces with confidence and precision. Whether you are optimizing gating geometry, riser placement, or pour temperature, RSM provides the analytical backbone to move from reactive firefighting to proactive, zero-defect decision-making.

Why RSM Fits Casting Reality — Not Just "More Data"
Casting is an inherently multi-variable, physics-intensive process. Engineers must simultaneously manage thermal gradients, fluid dynamics, solidification kinetics, and material behavior — all of which interact in nonlinear, often counterintuitive ways. Traditional "guess-and-check" trial runs are expensive, slow, and statistically unreliable. RSM replaces that approach with a structured, mathematically designed exploration of the process space, ensuring that every experiment — physical or virtual — delivers maximum information per unit of cost.
The Core Problem
Physical foundry trials are time-consuming and costly.
Each iteration of gating design, riser sizing, or pour temperature adjustment demands tooling modifications, material expenditure, and skilled labor hours.
Without a systematic methodology, engineers are essentially sampling a high-dimensional process space at random — missing critical interactions and leaving yield improvements on the table.
RSM reframes this challenge: instead of running hundreds of uncoordinated trials, you design a minimal, statistically optimal set of simulation runs that map the entire response landscape efficiently.
What RSM Delivers for Casting Teams
Structured Exploration
Design of Experiments principles ensure that simulation runs cover the process space systematically, capturing main effects and critical two-factor interactions without redundancy.
Defect Prediction Before Metal Flows
PoligonSoft's simulation platform generates shrinkage, porosity, and hot-tear risk maps that RSM converts into predictive regression models.
Decision-Ready Process Windows
Rather than a pile of uninterpreted simulation results, RSM delivers contour plots, optimal operating regions, and sensitivity rankings that engineering teams can act on immediately.
Accelerated Time-to-Market
By resolving defect risk virtually, teams dramatically compress the physical validation cycle, reducing scrap and rework costs across the production lifecycle.
RSM turns simulation outputs into a decision-ready map — not a pile of results. This is the operational promise of DoE-driven casting intelligence.
Casting is an inherently multi-variable, physics-intensive process. Engineers must simultaneously manage thermal gradients, fluid dynamics, solidification kinetics, and material behavior — all of which interact in nonlinear, often counterintuitive ways. Traditional "guess-and-check" trial runs are expensive, slow, and statistically unreliable. RSM replaces that approach with a structured, mathematically designed exploration of the process space, ensuring that every experiment — physical or virtual — delivers maximum information per unit of cost.
Effective RSM begins with a disciplined, domain-informed selection of input variables. In casting, the design space is vast — but experienced engineers and process parameter frameworks help identify the highest-leverage factors that drive defect formation, yield loss, and dimensional accuracy. The following four categories represent the primary variable families that should anchor any casting DoE study.
DoE Inputs — What You Actually Vary in the Foundry
Once DoE runs are executed in the casting simulator, RSM fits regression models to the resulting data, constructing mathematical surrogates that map every combination of inputs to predicted defect levels and performance metrics. This is where simulation data transforms from a collection of individual results into a navigable, continuous landscape of process knowledge.
Central Composite Design (CCD) and Box–Behnken Design (BBD) are the two workhorse experimental arrays for RSM in engineering applications. CCD augments a factorial core with axial "star" points to estimate curvature, making it ideal for processes with potentially nonlinear response behavior—which is the norm in casting.
The most powerful output of RSM is not the regression equation itself, but the contour and 3D response surface plots that make process tradeoffs instantly visible. Engineers can overlay multiple response surfaces—mapping feeding effectiveness against solidification time—to identify the region where all critical responses simultaneously meet their quality thresholds.
Build the Response Surface
Predict Defects & PerformanceCapture curvature with few simulation runs.
Map defects to input parameters.
statistically defensible process windows—
relied on by quality teams, process engineers, and customers.
RSM provides the analytical framework, but sustainable casting excellence requires embedding that framework into a repeatable, scalable digital infrastructure. The final step is operationalizing the simulation→RSM→decision loop so that every new casting design benefits automatically from accumulated process knowledge — without rerunning expensive full-physics simulations from scratch.
The true competitive advantage emerges when the simulation→RSM→decision loop becomes a standard operating procedure — not a one-off research exercise.
This means: versioned simulation databases that capture every DoE run and its RSM model, automated DoE generation scripts that initialize studies for new part families, and dashboards that surface process window boundaries to process engineers and quality teams in real time.
Teams that operationalize this infrastructure report dramatic reductions in physical trial iterations, faster new-part qualification cycles, and measurable improvements in first-pass yield — the ultimate measure of casting process intelligence.
Ready to move from reactive casting troubleshooting to proactive, RSM-powered process optimization? The path forward involves three concrete actions:
The foundry teams that master the simulation→RSM→decision loop will not just reduce defects today — they will build a compounding, self-improving process knowledge base that becomes a durable competitive advantage as part complexity and quality demands continue to escalate.
Step 3: Close the Loop — Fast Surrogates & Repeatable Digital Infrastructure
Operationalizing the Loop
Your Next Steps with RSM & PoligonSoft
What's Your Reaction?