Laminar-to-Turbulent Transition in Casting Systems
In metal casting, the difference between a flawless part and a scrapped one can come down to a single fluid dynamic threshold. Understanding how melt flow transitions from laminar to turbulent — and precisely when that shift occurs inside your gating system — is one of the most critical engineering levers available to a casting designer. This presentation breaks down the physics, the defect mechanisms, and the validation strategies that keep your fills predictable and your yields high.

Laminar Filling = Predictable,
Defect-Minimizing Flow
When the Reynolds Number (Re) remains below 2,000, molten metal moves through the gating system in an ordered, layered fashion — viscous forces dominate, inertial energy is damped, and the melt front advances predictably. This is the regime every casting engineer should be designing toward. At PoligonCast's engineering framework, laminar flow is treated as the non-negotiable baseline for high-integrity parts.
Why Laminar Flow Matters
In laminar conditions, each fluid layer slides past its neighbor with minimal energy exchange across boundaries.
The melt front remains continuous, oxide skins stay at the free surface where they belong, and gas entrapment events are virtually eliminated.
Wall shear stress stays low, protecting mold coatings and sand faces from mechanical erosion that could seed inclusions downstream.
Reynolds Number below 2,000 → viscous forces control the flow field
Ordered, parallel streamlines prevent oxide folding and bifilm initiation
Mold wall shear stress is minimized, protecting refractory and sand surfaces
Predictable thermal gradients enable reliable solidification modeling
Consistent fill time = consistent freeze pattern = repeatable mechanical properties
Engineering for the Laminar Regime
Achieving laminar fill is not accidental — it demands deliberate gating geometry, calculated runner cross-sections, and controlled pour rates.
The key variables are melt velocity at the ingate, hydraulic diameter of each runner segment, and the kinematic viscosity of the alloy at pouring temperature.
Even small geometry deviations — a sharp inside corner, an undersized sprue base, a mismatched runner transition — can elevate local Re above the 2,000 threshold and introduce defect seeds that propagate through the entire casting.
Proper tapered sprue design is foundational: a correctly tapered sprue maintains a full metal column, preventing aspiration of air that would immediately elevate effective Re by adding compressible phase to the melt stream.
Matching runner and ingate areas to designed fill rates closes the loop between process parameters and flow regime control.
Re < 2,000
Laminar — safe, predictable, defect-minimizing
Low Wall Shear
Minimal erosion risk; mold integrity preserved
Stable Front
Oxide skins stay surfaced; bifilm risk near zero
When the Reynolds Number (Re) remains below 2,000, molten metal moves through the gating system in an ordered, layered fashion — viscous forces dominate, inertial energy is damped, and the melt front advances predictably. This is the regime every casting engineer should be designing toward. At PoligonCast's engineering framework, laminar flow is treated as the non-negotiable baseline for high-integrity parts.
The transitional regime is the most treacherous zone in casting fluid dynamics — not because it produces the worst defects in isolation, but because the defects it creates are intermittent and statistically unpredictable. Parts produced in this regime can appear sound on visual inspection yet harbor sub-surface bifilms, micro-porosity clusters, and erosion-sourced inclusions that only emerge during machining, pressure testing, or in-service loading.
Learn more about how virtual validation of gating systems before production can help you identify and eliminate transitional flow conditions before metal ever hits the mold.
The Transitional Band (Re 2,000–4,000): Where Defects Become Random
Once Reynolds Number exceeds 4,000, inertial forces comprehensively override viscous damping. The melt flow field fractures into three-dimensional eddies, recirculation zones, and chaotic velocity vectors that bear no relationship to the designed runner geometry. At this point, defect generation is not a risk — it is a certainty. The engineering question shifts from prevention to damage limitation, and the answer is almost always: redesign before production, not rework after casting.
Reynolds Number at which inertia fully overrides viscous damping and turbulent defect generation becomes inevitable
Documented reduction in aluminum casting fatigue life at high bifilm densities from turbulent fill conditions
Jet impingement pressure multiplier versus laminar fill — the primary driver of sand erosion inclusion events
Number of reliable post-casting remediation methods for bifilms — prevention through flow control is the only answer
Turbulence (Re > 4,000): The Defects You Cannot Undo Later
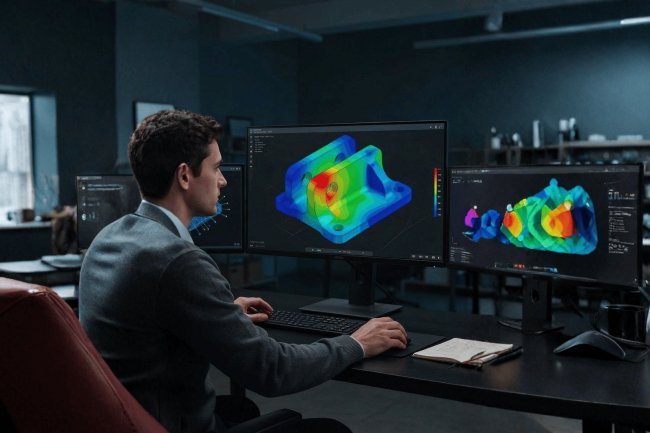
The most cost-effective point to control laminar-to-turbulent transition is before the first tool is cut and before the first metal is poured. Modern casting simulation platforms allow engineers to map Reynolds regimes across every segment of a gating system, identify geometry features that elevate local Re into the transitional or turbulent band, and iterate on runner design, taper ratios, and gate velocities — all in the digital domain. This approach replaces costly physical trial-and-error with targeted, physics-based design convergence. Explore PoligonCast's engineering capabilities to see how Reynolds-regime analysis is embedded into the design validation workflow from day one.
Local Re thresholds to watch: 2,000 and 4,000
Simulation captures transient melt velocity at every point in the gating system throughout the fill event — not just at steady state. Engineers can visualize exactly when and where local Re crosses the 2,000 and 4,000 thresholds, which specific geometry features are responsible, and how those zones evolve as fill progresses and melt temperature drops. Thermal gradient mapping overlaid with flow data reveals solidification timing that would otherwise only be discovered through costly physical trials and destructive sectioning.
Virtual validation of gating systems makes this analysis available at the design stage, where changes cost engineering hours rather than tooling dollars.
Once simulation identifies the Re distribution across the gating system, engineers can set quantitative process targets: maximum pour rate to maintain Re < 2,000 at the critical ingate, minimum runner cross-section to avoid velocity spikes at direction changes, corner radius minima to prevent boundary layer separation.
These targets are traceable, documentable, and auditable — transforming flow control from an empirical art into an engineering specification. This is particularly valuable for aerospace, automotive structural, and pressure-tight applications where process capability documentation is a customer or regulatory requirement.
A single physical casting trial — including tooling modification, production scheduling, metal cost, labor, and destructive evaluation — typically costs orders of magnitude more than a simulation iteration. Virtual validation compresses the design loop: an engineer can evaluate five gating geometry variants in the time it takes to schedule one physical pour.
The result is not just cost savings but better outcomes — simulation explores the design space more completely than physical trials, catching regime transitions that would only manifest in edge-case process conditions unlikely to be captured during limited physical validation runs.
The laminar-to-turbulent transition is not a materials problem or a metallurgy problem — it is a fluid dynamics problem with a geometry solution. Design the flow path first; the metallurgy follows.
Start with PoligonCast's engineering overview to understand how Reynolds-aware gating design is applied across alloy systems and casting processes.
Prevent the Transition Using Virtual Validation Before Production
Map Fill Behavior Across Thermal and Flow Regimes
Apply Reynolds-Regime Logic to Set Defensible Process Targets
Replace Physical Trials with Targeted Digital Iteration
What's Your Reaction?